
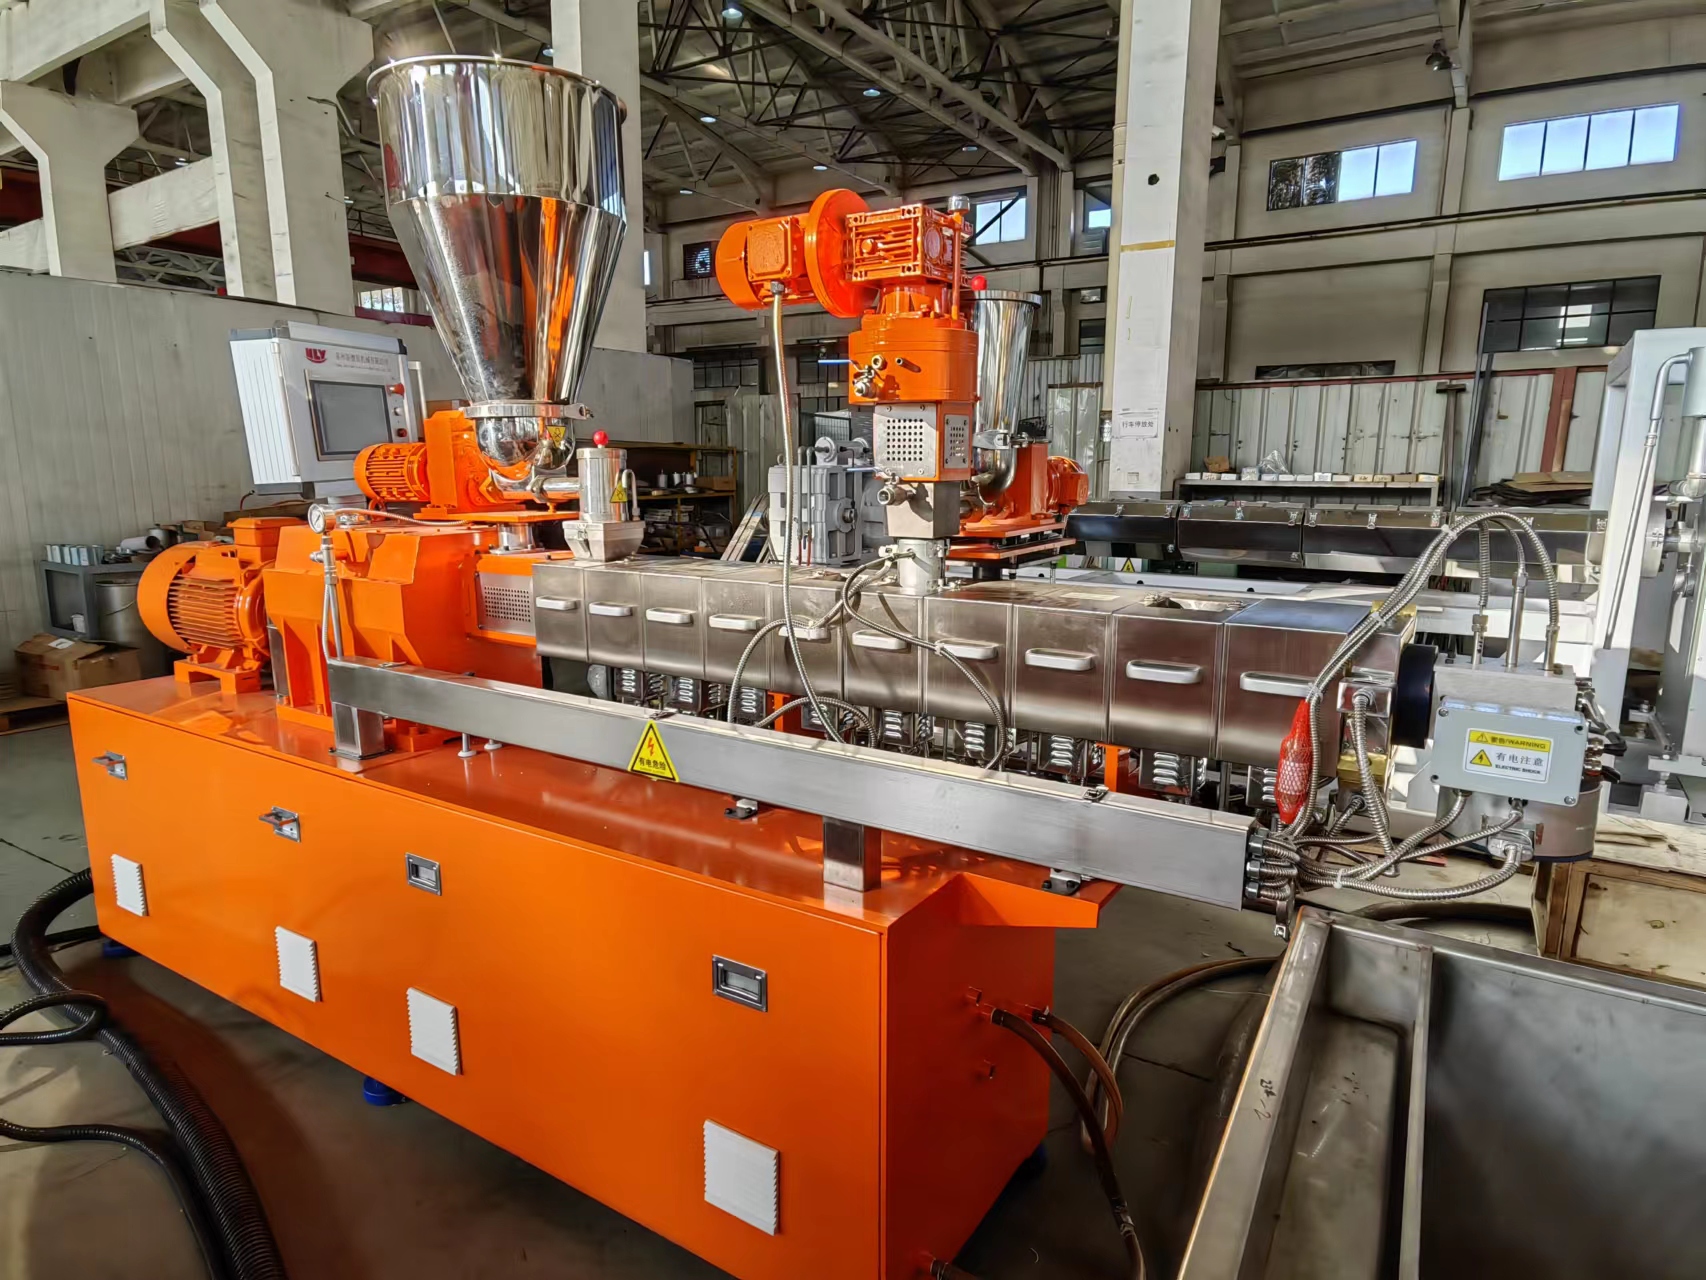
Meta Title: Monofilament Extrusion Machine: Process, Components, Materials & Buying Guide
Meta Description: Learn how a monofilament extrusion machine works, including material drying, extrusion, melt filtration, quenching, drawing, heat setting and winding. Compare PET, PA, PP and HDPE processing requirements and learn how to choose the right monofilament extrusion line.
URL Slug: /monofilament-extrusion-machine-guide/
Quick Answer
A monofilament extrusion machine is a complete production system used to convert polymer raw materials into continuous plastic monofilaments with controlled diameter, tensile strength, shape, surface quality and dimensional stability.
Although people often use the term “monofilament extruder” or “monofilament extrusion machine” to describe the equipment, a complete production line includes much more than a single extruder.
A typical monofilament extrusion line follows this process:
Raw Material Preparation → Drying → Extrusion → Melt Filtration → Melt Metering → Spinneret Die → Water Quenching → Drawing → Heat Setting → Surface Treatment → Winding
Depending on the material and application, a monofilament extrusion machine can process polymers such as:
- PET
- PA6
- PA66
- PA612
- PP
- HDPE
- PBT
The finished monofilament can be used for:
- Toothbrush bristles
- Broom filaments
- Cleaning brush filaments
- Paint brush filaments
- Industrial brush filaments
- Rope
- Fishing products
- Zipper monofilament
- Artificial grass
- Agricultural products
- Industrial mesh
- Other customized plastic monofilament applications
Important: Process temperatures, draw ratios, production output and achievable tolerances depend on the polymer grade, filament diameter, additives, equipment configuration and final application. Typical engineering ranges should not be treated as universal settings.
Key Facts About Monofilament Extrusion Machines
Item | Description |
Machine Type | Plastic monofilament extrusion line |
Main Function | Converts polymer pellets into continuous monofilament |
Main Materials | PET, PA, PP, HDPE, PBT and customized polymers |
Core Process | Extrusion → Cooling → Drawing → Heat Setting → Winding |
Key Quality Factors | Diameter, ovality, tensile strength, elongation, shrinkage and surface quality |
Typical Applications | Brushes, brooms, ropes, zippers, fishing products, artificial grass and industrial products |
Configuration | Customized according to material, diameter, output and application |
What Is the Difference Between a Monofilament Extruder and a Complete Monofilament Extrusion Line?
A single extruder is only one part of the production process.
Its primary function is to melt and convey the polymer.
A complete monofilament extrusion line performs the entire manufacturing process required to transform polymer pellets into finished filament.
Equipment | Main Function |
Raw Material System | Feeds and prepares polymer |
Dryer | Removes moisture when required |
Single-Screw Extruder | Melts and homogenizes polymer |
Melt Filter | Removes contamination |
Gear Melt Pump | Stabilizes melt flow |
Spinneret Die | Forms continuous filaments |
Water Quench Tank | Cools and solidifies filaments |
Drawing Unit | Orients polymer molecules |
Heat-Setting Unit | Stabilizes filament dimensions |
Surface Treatment Unit | Adds oiling, antistatic treatment or crimping |
Winder | Collects finished filament |
Complete Extrusion Line | Integrates all stages into one synchronized process |
This distinction is important when comparing suppliers.
A monofilament extrusion line should be evaluated as an integrated process system, not simply as a collection of individual machines.
The stability of the final filament depends on the interaction between:
- Melt pressure
- Melt temperature
- Die performance
- Quench conditions
- Drawing speed
- Draw ratio
- Heat-setting conditions
- Winding tension
A problem in one section of the line can affect the quality of the finished monofilament.
How Does a Monofilament Extrusion Machine Work?
A monofilament extrusion machine works by converting polymer pellets into continuous filaments through a sequence of controlled thermal and mechanical processes.
Step 1: Prepare and Dry the Raw Material
The production process starts with raw material preparation.
Some polymers absorb moisture from the atmosphere and require careful drying before entering the extruder.
PET and nylon materials are especially sensitive to moisture. Excess moisture can cause polymer degradation during melting and may result in:
- Brittle filament
- Surface bubbles
- Reduced mechanical properties
- Unstable processing
- Frequent filament breakage
PET and nylon may require a closed-loop dehumidifying dryer.
PP and HDPE are generally less hygroscopic and may require different preparation conditions.
The correct drying process depends on the specific polymer grade and material supplier recommendations.
Main purpose: Prepare the polymer for stable melting and extrusion.
Step 2: Melt and Homogenize the Polymer
After preparation, the raw material enters the single-screw extruder.
The rotating screw performs several functions:
- Conveys the polymer forward
- Compresses the material
- Melts the polymer
- Mixes the polymer
- Homogenizes the melt
- Delivers the melt to downstream equipment
Monofilament extrusion applications commonly use single-screw extruders designed to provide stable melt quality.
A typical screw design may use an L/D ratio around 30:1, although the final screw specification should be matched to the polymer and production requirements.
The extruder barrel is usually divided into multiple temperature control zones.
Stable temperature control is important because temperature variation can change polymer viscosity, which may eventually affect:
- Melt pressure
- Melt flow
- Filament diameter
- Surface quality
- Process stability
Main purpose: Produce a stable and homogeneous polymer melt.
Step 3: Filter and Meter the Polymer Melt
After leaving the extruder, the molten polymer can pass through a melt filtration system.
The filtration system helps remove:
- Contamination
- Carbonized particles
- Foreign material
- Degraded polymer
- Impurities from recycled material
This stage becomes especially important when processing recycled raw materials.
After filtration, the melt may pass through a gear melt pump.
A gear pump is used to provide more stable volumetric melt delivery.
The screw extruder creates the melt, but a gear pump can help improve flow consistency before the polymer reaches the spinneret die.
Main purpose: Improve melt cleanliness and stabilize melt delivery.
Step 4: Form the Filament Through the Spinneret Die
The polymer melt enters the spinneret die head.
The die distributes the melt and forms the initial filament shape through precision die holes.
Depending on the production requirements, the die may produce different numbers of filaments.
The die design can influence:
- Filament diameter
- Filament shape
- Number of production ends
- Initial filament roundness
- Production capacity
Different die designs can also be used for:
- Round monofilament
- Hollow monofilament
- Profiled filament
- Customized cross-sections
Main purpose: Convert molten polymer into continuous filament strands.
Step 5: Quench and Solidify the Filament
After leaving the spinneret die, the hot polymer strands enter a controlled cooling zone.
A stainless-steel water quench tank is commonly used.
The cooling process solidifies the polymer and prepares the filament for downstream drawing.
Quench conditions can affect:
- Initial filament geometry
- Surface quality
- Roundness
- Diameter stability
- Drawing performance
Water temperature and water flow should be controlled according to the polymer and product requirements.
Typical industrial quench water ranges may fall within approximately 15–35°C, but the correct temperature depends on the material and process.
Stable and uniform water flow is important.
Uncontrolled turbulence or uneven cooling may affect the consistency of the filament.
Main purpose: Solidify the filament while maintaining stable initial geometry.
Step 6: Draw and Orient the Polymer
Drawing is one of the most important stages in monofilament production.
After cooling, the polymer chains inside the filament are not yet fully oriented.
The filament passes through synchronized rollers or godets operating at different speeds.
The speed difference creates a draw ratio.
During drawing, the filament is stretched and the polymer molecules become more aligned along the length of the filament.
This process can significantly improve:
- Tensile strength
- Molecular orientation
- Diameter control
- Mechanical performance
Typical total draw ratios vary according to the polymer.
Depending on the material and product requirements, monofilament drawing may use:
- Heated water
- Hot-water tanks
- Hot-air ovens
- Other controlled heating systems
The drawing system must maintain stable synchronization.
If roller speeds are unstable or improperly matched, the final filament diameter may fluctuate.
Main purpose: Increase strength and control the final filament structure and diameter.
How Does Drawing Affect Filament Diameter?
The relationship between melt output and drawing speed is one of the fundamental principles of monofilament diameter control.
General principle:
Higher melt output + constant line speed = larger filament diameter
Constant melt output + higher drawing speed = smaller filament diameter
However, actual production is more complex.
Final diameter is also affected by:
- Polymer viscosity
- Melt temperature
- Melt pressure
- Die geometry
- Quenching conditions
- Draw ratio
- Polymer relaxation
- Winding tension
For this reason, modern monofilament extrusion lines benefit from synchronized drive systems and inline quality monitoring.
Step 7: Heat Set and Anneal the Filament
Drawing creates molecular orientation, but it can also leave internal stress inside the polymer.
If the filament is wound immediately without sufficient stabilization, it may shrink or deform during later processing.
The heat-setting stage is designed to improve dimensional stability.
The filament passes through a controlled heating zone while the line maintains appropriate tension and relaxation conditions.
Depending on the material, the process may use:
- Hot-air ovens
- Heated chambers
- Controlled godet systems
- Other thermal stabilization equipment
Heat-setting conditions vary by polymer.
Typical temperature ranges can differ significantly between HDPE, PP, nylon and PET.
The correct setting should be determined according to the material grade and product performance requirements.
Main purpose: Reduce internal stress and improve dimensional stability.
Step 8: Apply Surface Treatment When Required
Not every monofilament product requires additional surface treatment.
However, many brush and specialty filament applications may use finishing equipment.
Common options include:
Antistatic Oiling
A controlled amount of finishing agent is applied to the filament.
This can help:
- Reduce static
- Reduce friction
- Improve handling
- Improve downstream processing
Gear Crimping
Some brush filaments require a crimped shape.
A crimping system can modify the filament structure to create specific physical characteristics.
Other Customized Treatments
Depending on the final application, the production line may also include customized surface treatment systems.
Main purpose: Improve handling and application-specific performance.
Step 9: Wind the Finished Monofilament
The final production stage is winding.
The finished filament is collected onto spools, bobbins or other packages.
Winding tension must remain stable as the package diameter increases.
Poor winding control can create problems such as:
- Loose packages
- Package collapse
- Filament deformation
- Unstable unwinding
- Downstream processing difficulties
Modern winding systems may use independent motors or servo-based control systems.
Main purpose: Produce a stable and usable finished filament package.
Monofilament Extrusion Process: Input, Process and Output
Production Stage | Input | Process | Output |
Material Preparation | Polymer pellets | Conditioning and drying | Prepared resin |
Extrusion | Prepared resin | Melting and homogenization | Polymer melt |
Filtration | Polymer melt | Removal of contamination | Clean melt |
Metering | Clean melt | Controlled melt delivery | Stable melt flow |
Spinning | Stable melt | Filament formation through die | Initial filaments |
Quenching | Hot filaments | Controlled cooling | Solidified strands |
Drawing | Solidified strands | Molecular orientation | High-strength filament |
Heat Setting | Drawn filament | Thermal stabilization | Dimensionally stable filament |
Surface Treatment | Finished filament | Oiling, crimping or other treatment | Application-ready filament |
Winding | Finished filament | Tension-controlled collection | Final package |
What Materials Can a Monofilament Extrusion Machine Process?
A monofilament extrusion line can be configured for different polymer materials.
However, the same processing conditions are not suitable for every polymer.
The machine configuration may need to change depending on:
- Dryer requirements
- Extruder design
- Temperature range
- Screw design
- Filtration requirements
- Drawing conditions
- Heating method
- Heat-setting capacity
- Winding requirements
The most common materials include PET, nylon, PP and HDPE.
Can a Monofilament Extrusion Machine Process PET?
Yes.
PET is widely used in monofilament production.
PET processing generally requires careful moisture control before extrusion.
The material must then be melted, formed, cooled, drawn and heat-set under controlled conditions.
PET monofilament can be selected for applications requiring specific combinations of:
- Strength
- Stiffness
- Dimensional stability
- Surface quality
The final process configuration depends on the PET grade and finished filament requirements.
Can a Monofilament Extrusion Machine Process Nylon?
Yes.
Common monofilament materials include:
- PA6
- PA66
- PA612
Nylon materials are hygroscopic and generally require strict moisture control.
Processing conditions can vary significantly between different nylon grades.
Nylon monofilament is commonly selected for applications requiring specific mechanical properties such as strength, flexibility or abrasion resistance.
The dryer, extrusion temperature profile, drawing conditions and heat-setting system should be selected according to the exact nylon grade.
Can a Monofilament Extrusion Machine Process PP?
Yes.
PP monofilament is widely used for various industrial and consumer applications.
PP offers a relatively low material density and can be used for products requiring particular combinations of:
- Lightweight performance
- Chemical resistance
- Flexibility
- Production efficiency
PP processing conditions differ from PET and nylon.
The complete line should be configured around the specific PP grade and product requirements.
Can a Monofilament Extrusion Machine Process HDPE?
Yes.
HDPE can be used for monofilament applications requiring specific combinations of flexibility and chemical resistance.
HDPE drawing behavior can differ significantly from other polymers.
The cooling system, drawing ratio and heat-setting conditions should therefore be selected for the specific material and finished product.
Typical Material Processing Overview
Polymer | Typical Melt Processing Range | Typical Draw Ratio | Typical Heat-Setting Range |
PA6 / PA66 / PA612 | Approx. 240–300°C depending on grade | Approx. 4.5:1–5.8:1 | Approx. 170–200°C |
PET | Approx. 260–300°C depending on grade | Approx. 4.8:1–6.2:1 | Approx. 180–220°C |
PP | Approx. 200–280°C depending on grade | Approx. 5.0:1–7.0:1 | Approx. 130–150°C |
HDPE | Approx. 235–285°C depending on grade | Approx. 8.0:1–10.0:1 | Approx. 110–125°C |
PBT | Approx. 230–250°C depending on grade | Application-dependent | Application-dependent |
Note: These are typical engineering ranges only. Actual process settings must be determined according to the specific resin grade, additives, filament diameter, output and end-use requirements.
What Determines Monofilament Diameter?
Monofilament diameter is controlled by the balance between polymer output and downstream line speed.
The most important factors include:
- Melt pressure stability
- Melt temperature stability
- Polymer viscosity
- Gear pump consistency
- Die hole geometry
- Quench temperature
- Water flow stability
- Drawing speed
- Draw ratio
- Heat-setting conditions
- Winding tension
For high-precision applications, inline measurement can provide continuous diameter feedback.
A laser measurement system can monitor the filament during production and provide data to the control system.
Depending on the equipment configuration, the system may adjust process variables to reduce diameter variation.
Applications requiring very tight tolerances may use advanced inline measurement and closed-loop control.
How Is Monofilament Quality Controlled?
Monofilament quality should not be evaluated by diameter alone.
Important quality indicators can include:
- Diameter
- Diameter tolerance
- Ovality
- Tensile strength
- Elongation
- Thermal shrinkage
- Surface smoothness
- Color consistency
- Filament straightness
- Package quality
A stable production line should control quality across the entire process.
Layer 1: Melt Stability
Stable melt temperature and pressure help maintain consistent polymer flow.
Layer 2: Cooling Stability
Uniform quenching helps maintain filament geometry and surface quality.
Layer 3: Drawing Stability
Synchronized drive systems help maintain consistent orientation and diameter.
Layer 4: Inline Measurement
Laser gauges or other measuring systems can monitor the product continuously.
Layer 5: Winding Stability
Controlled tension helps protect the finished filament during package formation.
Common Monofilament Extrusion Problems and Their Possible Causes
Why Is My Filament Diameter Unstable?
Possible causes include:
- Unstable melt pressure
- Melt temperature variation
- Inconsistent polymer viscosity
- Contaminated filter screens
- Gear pump instability
- Uneven quench conditions
- Drawing speed variation
- Drive synchronization problems
The first step should be to identify where the variation begins.
Do not assume the problem is caused only by the extruder.
A monofilament production line is an integrated system.
Why Does Monofilament Break During Drawing?
Possible causes include:
- Excessive draw ratio
- Incorrect heating conditions
- Moisture in the raw material
- Polymer degradation
- Surface defects
- Unstable roller speed
- Incorrect tension
- Poor initial filament quality
The solution should be based on process data rather than simply reducing line speed.
Why Does the Filament Have Bubbles?
Possible causes include:
- Excessive raw material moisture
- Insufficient drying
- Polymer degradation
- Contamination
- Unstable processing temperature
Hygroscopic materials should be checked carefully for moisture-related problems.
Why Is the Filament Oval Instead of Round?
Possible causes include:
- Die problems
- Uneven cooling
- Unstable tension
- Incorrect drawing conditions
- Uneven downstream pulling
The spinneret, quench system and drawing system should all be inspected.
Why Does the Finished Filament Shrink?
Excessive shrinkage may be caused by:
- Insufficient heat setting
- Excessive internal orientation stress
- Incorrect relaxation conditions
- Material-specific processing problems
The thermal stabilization process should be reviewed.
Why Is the Filament Surface Rough?
Possible causes include:
- Melt contamination
- Carbonized material
- Damaged die surfaces
- Poor filtration
- Material degradation
- Unstable cooling
The melt filtration system and spinneret condition should be inspected.
What Applications Use Monofilament Extrusion Machines?
A customized monofilament extrusion line can be designed for many different products.
Brush and Bristle Production
Applications include:
- Toothbrush filament
- Cleaning brush filament
- Industrial brush filament
- Paint brush filament
- Cosmetic brush filament
Broom Filament Production
Broom monofilament can be produced with customized requirements for:
- Diameter
- Stiffness
- Crimping
- Color
- Surface treatment
Rope Production
Monofilament may be used as a raw material for different rope products.
The line configuration depends on the material, diameter and required mechanical performance.
Zipper Monofilament Production
Zipper applications may require controlled dimensional stability and specific material characteristics.
Fishing Products
Monofilament can be produced for selected fishing and related applications.
Artificial Grass and Agricultural Applications
Certain plastic filament products can be used in artificial grass and agricultural applications.
Industrial Products
Customized monofilament can also be used for:
- Industrial mesh
- Filter-related applications
- Technical products
- Specialized plastic components
How to Choose the Right Monofilament Extrusion Machine
The correct machine should not be selected only according to price.
The production line should first be matched to the actual product.
Before requesting a quotation, identify:
- Raw material
- Filament diameter
- Filament shape
- Required output
- Number of production ends
- Final application
- Quality requirements
- Factory space
- Power supply
- Automation requirements
The most important selection principle is:
Material + Filament Specification + Required Output + Final Application = Machine Configuration
10 Questions to Ask Before Buying a Monofilament Extrusion Machine
1. What materials can the line process?
Confirm the exact polymer grades the equipment is designed to handle.
2. What filament diameter range can the machine produce?
Ask for the actual production range rather than a general machine description.
3. What output can be achieved for my specific product?
Output depends on material, diameter, number of ends and process conditions.
4. What diameter tolerance can be achieved?
Ask for performance information based on your actual material and filament specification.
5. Is a gear melt pump included?
For applications requiring stable melt delivery, a gear pump may be an important part of the configuration.
6. Is inline diameter measurement available?
Continuous monitoring can be valuable for high-precision products.
7. How are the drawing units synchronized?
Stable drawing depends on accurate speed coordination.
8. What is the energy consumption?
Compare suppliers using specific energy consumption whenever possible.
9. Can the supplier perform a factory acceptance test?
A FAT using the correct material and target specification can provide valuable production data.
10. What after-sales support is available?
Confirm:
- Warranty scope
- Spare parts
- Remote support
- Installation support
- Commissioning support
- Operator training
How Should You Compare Monofilament Extrusion Machine Suppliers?
A useful supplier comparison should evaluate the complete process rather than only the initial equipment price.
Evaluation Area | Question to Ask | What to Look For |
Diameter Precision | What tolerance can you achieve? | Performance data based on actual requirements |
Process Stability | How is melt and line stability controlled? | Stable melt delivery and synchronized drives |
Energy Efficiency | What is the specific energy consumption? | Documented production data |
Equipment Quality | What components are used? | Durable and serviceable equipment |
Automation | What process monitoring is included? | Practical control and measurement systems |
After-Sales Support | How quickly can support be provided? | Clear service process and spare parts support |
Total Cost of Ownership | What will the line cost over time? | Energy, maintenance, scrap and downtime considerations |
Why Total Cost of Ownership Matters More Than Machine Price
The purchase price is only one part of the investment.
The total cost of operating a monofilament extrusion line may include:
- Electricity
- Raw material waste
- Scrap
- Rework
- Maintenance
- Wear parts
- Downtime
- Spare parts
- Operator training
When comparing multiple suppliers, consider the complete operating cost over several years.
Useful questions include:
- How many kWh are required per kilogram of finished filament?
- How much scrap is generated during normal operation?
- How quickly can the machine return to stable production after a process change?
- How long do major wear components last?
- How easily can spare parts be replaced?
- How quickly can technical support be provided?
A lower initial machine price does not always mean a lower long-term production cost.
Frequently Asked Questions About Monofilament Extrusion Machines
What is a monofilament extrusion machine?
A monofilament extrusion machine is a production system that converts polymer materials into continuous plastic filaments through extrusion, cooling, drawing, heat setting and winding.
How does a monofilament extrusion line work?
The line prepares the raw material, melts the polymer, filters and meters the melt, forms filaments through a die, cools them, draws them to orient the polymer molecules, heat-sets them and finally winds the finished filament.
What is the difference between an extruder and an extrusion line?
An extruder melts and conveys polymer. A complete extrusion line includes the extruder plus the downstream equipment required to produce finished monofilament.
What materials can be used?
Common materials include PET, PA6, PA66, PA612, PP, HDPE and PBT.
Can one production line process multiple materials?
A line can be designed for multiple materials, but the configuration may need to accommodate different drying, temperature, drawing and heat-setting requirements.
What determines monofilament diameter?
Diameter is affected by melt output, line speed, drawing conditions, die geometry, cooling stability and other process variables.
Why is a gear pump used?
A gear pump can help provide more stable volumetric melt delivery between the extruder and spinneret die.
Why do PET and nylon require drying?
These materials can absorb moisture. Excess moisture may contribute to polymer degradation and processing defects.
What causes filament breakage?
Possible causes include excessive draw ratio, incorrect heating, material moisture, polymer degradation, surface defects and unstable process conditions.
What causes diameter variation?
Common causes include unstable melt pressure, temperature variation, filtration problems, quench instability and drawing speed variation.
How is monofilament strength increased?
Drawing stretches the filament and helps orient polymer molecules along the filament axis.
Why is heat setting necessary?
Heat setting helps reduce internal stress and improve dimensional stability.
What information is needed before requesting a quotation?
The supplier should know the material, filament diameter, output requirement, final application, number of filaments and special processing requirements.
About NLY Monofilament Extrusion Technology
Changzhou New Liaoyuan Machinery Co., Ltd. (NLY) specializes in plastic monofilament extrusion equipment and customized monofilament production line solutions.
Our equipment can be configured according to the processing requirements of different polymers and monofilament products.
A customized production line may include:
- Raw material feeding
- Material drying
- Single-screw extrusion
- Melt filtration
- Gear melt pumping
- Precision spinneret dies
- Water quenching
- Multi-stage drawing
- Heat setting
- Annealing
- Surface treatment
- Oiling
- Crimping
- Automatic winding
- PLC-based process control
- Optional inline diameter monitoring
The final equipment configuration should be determined according to the actual production requirements rather than a generic machine specification.
Request a Custom Monofilament Extrusion Line Proposal
To recommend the correct monofilament extrusion machine configuration, please provide the following information:
- Raw Material
PET, PA6, PA66, PA612, PP, HDPE, PBT or another polymer - Filament Diameter
Minimum and maximum diameter requirements - Filament Shape
Round, hollow, profiled or customized - Required Production Capacity
kg/hour, kg/day or other production target - Number of Filaments
Required production ends or die holes - Final Application
Brush, broom, rope, zipper, fishing product, artificial grass or another product - Special Requirements
Crimping, oiling, antistatic treatment, color, recycled material or other requirements - Power Supply
Voltage, frequency and phase - Factory Layout
Available installation space - Quality Requirements
Required tolerance, strength, shrinkage or other product specifications
Based on this information, a monofilament extrusion line can be designed around the actual production process and product requirements.
Conclusion
A monofilament extrusion machine should be understood as a complete and synchronized production system rather than a standalone extruder.
Stable monofilament production depends on the coordination of material preparation, extrusion, melt delivery, die design, cooling, drawing, heat setting and winding.
The best equipment configuration depends on four core factors:
Raw Material + Filament Specification + Required Output + Final Application
Before investing in a new production line, evaluate the complete process, verify the supplier’s ability to meet your actual specifications and compare total cost of ownership rather than only the initial machine price.
For a customized monofilament extrusion line proposal, provide your material, filament diameter, production capacity and final application to receive a machine configuration designed around your actual manufacturing requirements.







