
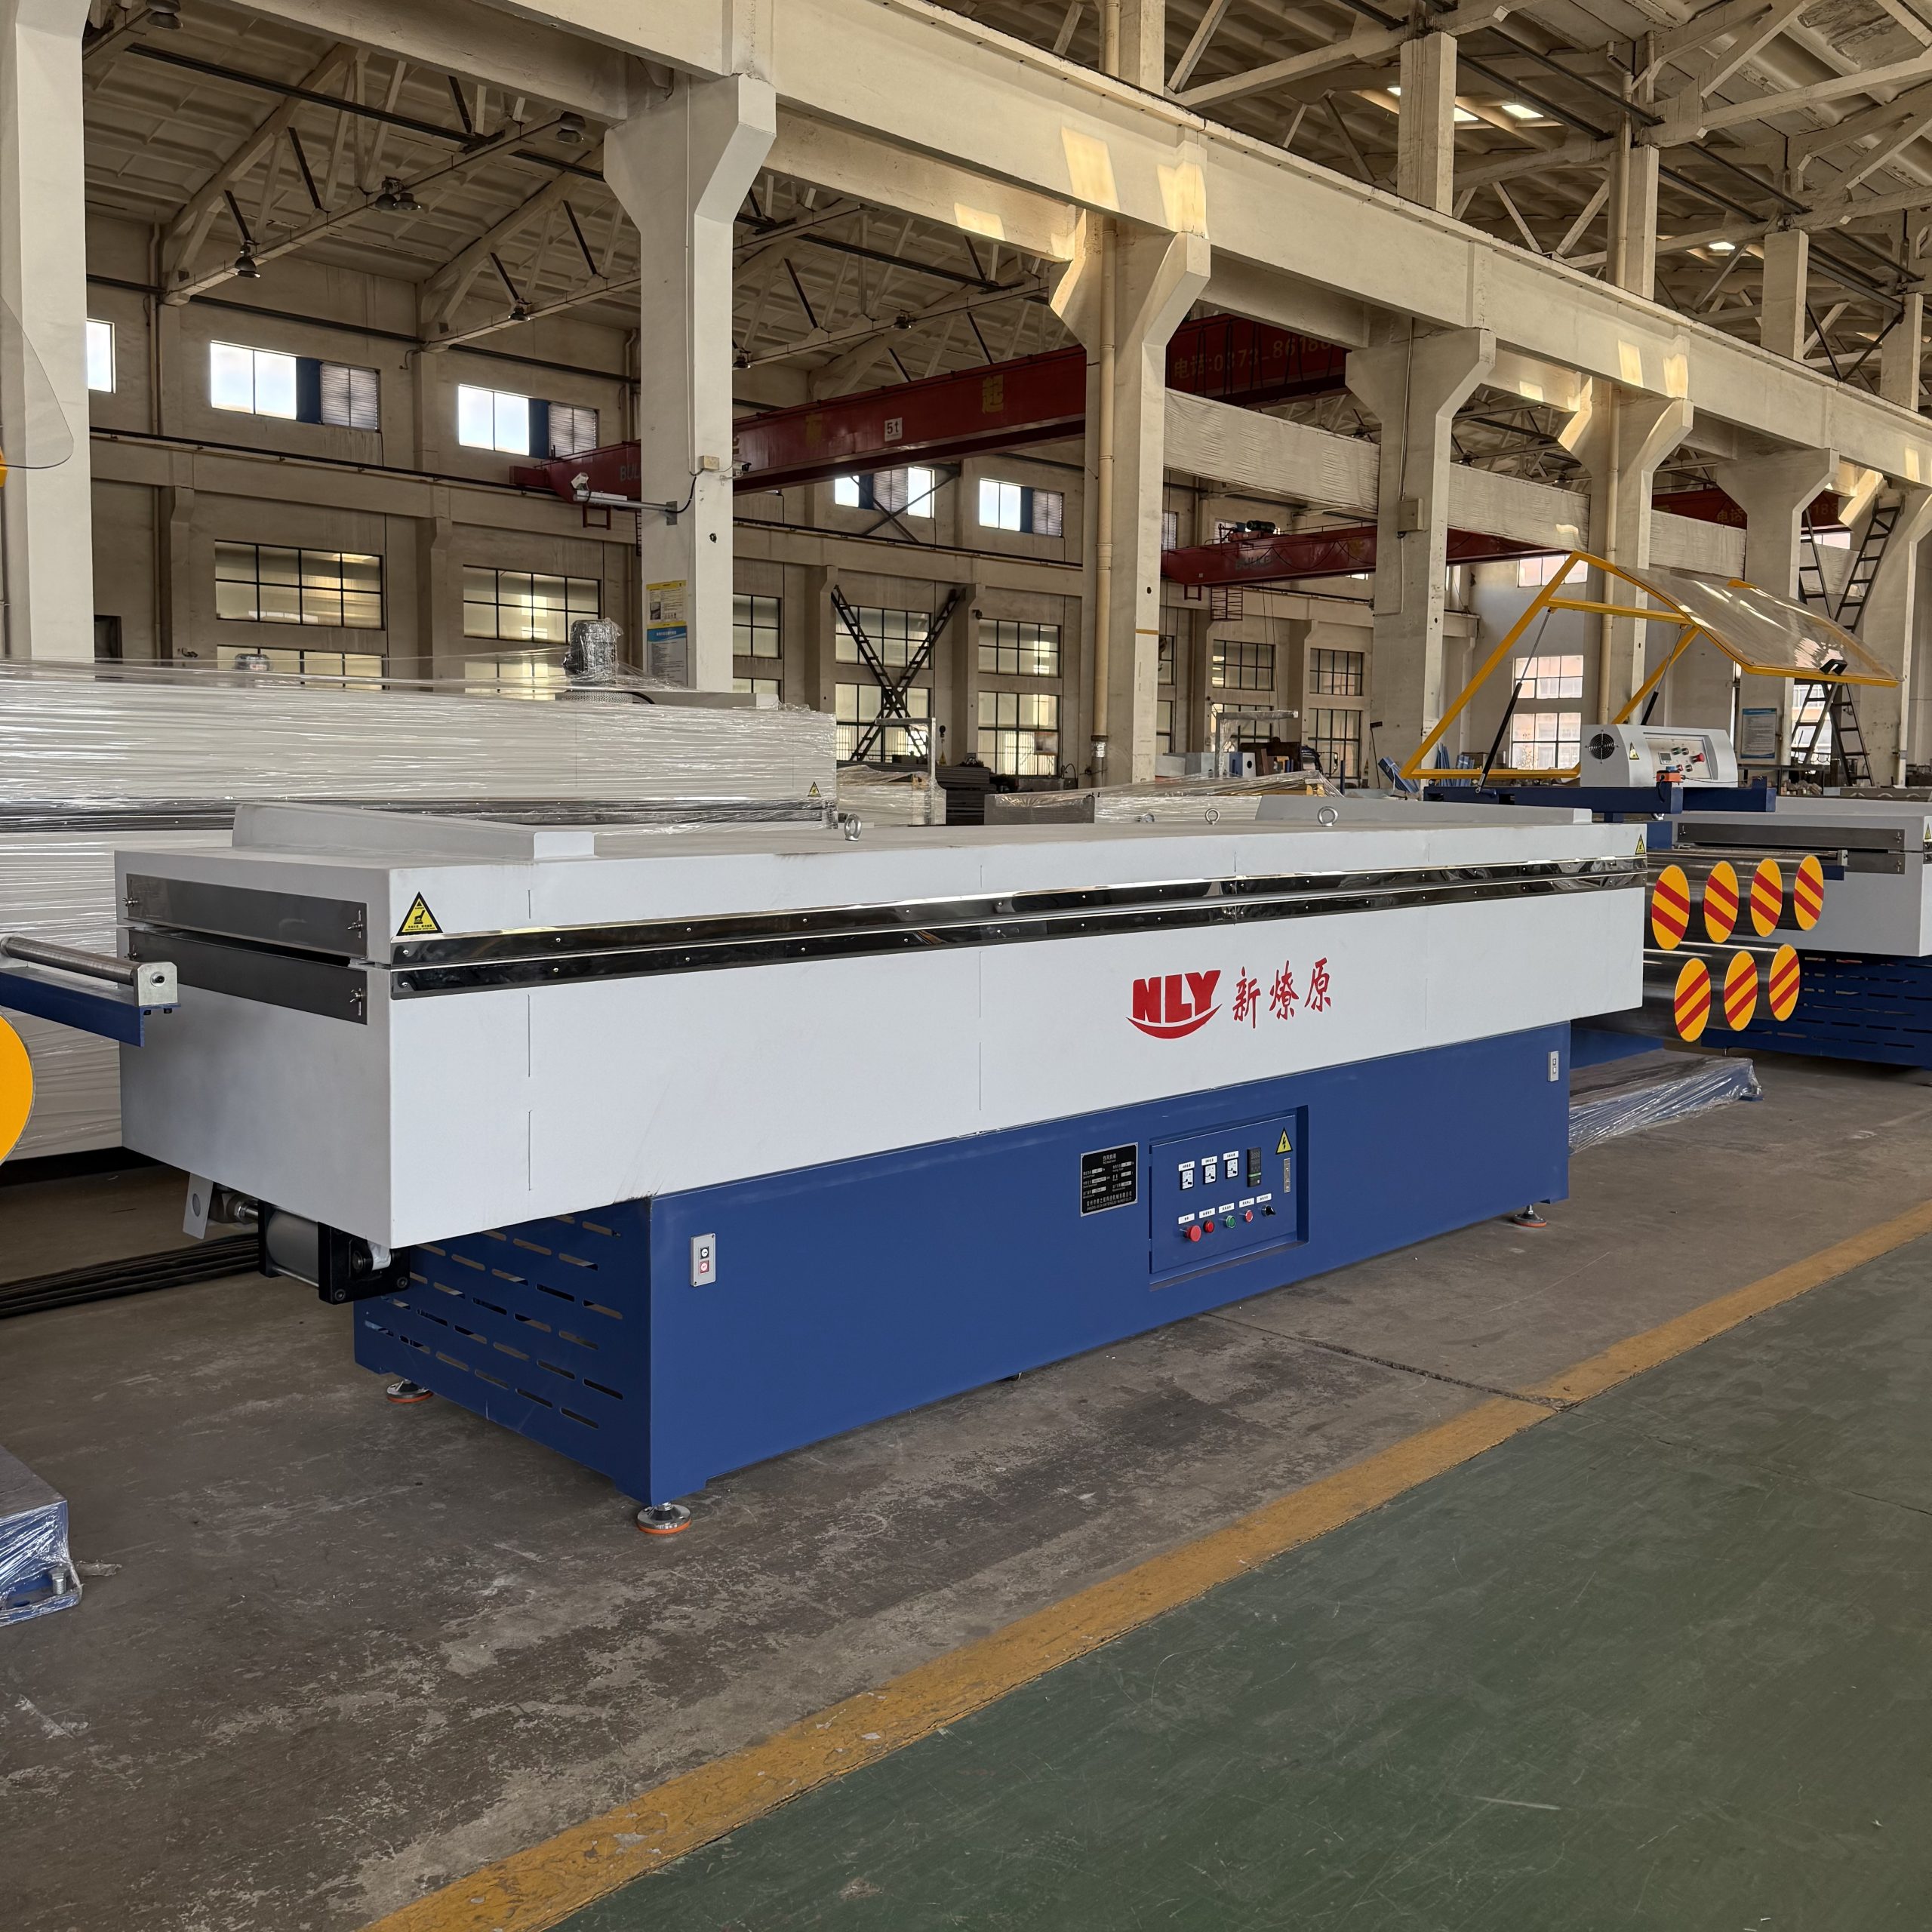
Choosing a monofilament extrusion machine is not simply a matter of comparing extruder size, motor power, or advertised output.
The right machine must match four fundamental production requirements:
Polymer → Filament Diameter → Production Output → End-Use Application
These inputs determine the appropriate screw diameter, L/D ratio, screw design, temperature-control system, die configuration, drawing system, annealing method, winding system, and automation level.
A machine with a higher theoretical output is not necessarily the better choice. For monofilament production, the more important question is whether the complete line can maintain the required diameter, ovality, tensile strength, elongation, surface quality, and production stability at the target output.
This guide explains how to evaluate a monofilament extrusion machine from a technical and purchasing perspective.
Quick Answer: How Do You Choose a Monofilament Extrusion Machine?
The selection process should begin with the final filament specification rather than the extruder model.
Before requesting a quotation, define:
- Polymer— PA6, PA66, PET, PP, PE/HDPE, or another resin
- Resin condition— virgin, recycled, or blended material
- Finished filament diameter— minimum, maximum, and target diameter
- Diameter tolerance and ovality requirement
- Production output— kg/h under actual production conditions
- End-use application— brush, broom, zipper, fishing line, rope, mesh, synthetic grass, or industrial filament
- Mechanical requirements— tensile strength, elongation, stiffness, rebound, or other product-specific requirements
- Winding/package format
- Required automation and diameter monitoring
Once these requirements are defined, the supplier can determine the appropriate extruder size and downstream configuration.
The extruder should be selected from the product requirements backward, not from a standard machine model forward.
What Is a Monofilament Extrusion Machine?
A monofilament extrusion machine is a production system that melts thermoplastic polymer, forms continuous filaments through a die or spinneret, cools and draws the filaments, heat-sets their properties, and winds the finished monofilament.
A complete monofilament extrusion line normally includes:
Raw Material Preparation → Extrusion → Melt Filtration → Die/Spinneret → Quenching → Drawing → Heat Setting/Annealing → Oil Treatment → Winding
The extruder is only one part of this system.
The extruder generates and stabilizes the polymer melt.
The downstream system determines much of the final filament’s:
- Diameter
- Tensile strength
- Elongation
- Stiffness
- Molecular orientation
- Dimensional stability
- Package quality
This distinction is important during machine purchasing.
A diameter problem may appear after drawing, but the root cause can originate in the extrusion section. Conversely, an extrusion system can be stable while diameter variation is caused by cooling, drawing, roller synchronization, or winding tension.
Therefore, a monofilament line should be evaluated as one integrated process rather than a collection of independent machines.
The Five Production Inputs You Should Define First
Before comparing suppliers, define the production requirements.
These five inputs have the greatest influence on the final machine configuration.
1. Polymer and Resin Condition
Different polymers require different extrusion conditions.
Common monofilament materials include:
- PA6
- PA66
- PET
- PP
- PE
- HDPE
- PBT
- Polymer blends
- Recycled polymers
The resin condition is equally important.
Specify whether the production uses:
- Virgin pellets
- Recycled pellets
- PET flakes
- Post-industrial recycled material
- Polymer blends
- Material containing additives
Why does this matter?
Polymer selection affects:
- Screw geometry
- Barrel temperature
- Drying system
- Melt filtration
- Screw and barrel wear
- Drawing conditions
- Die design
- Final mechanical properties
For example, PET, PA6, and PA66 are moisture-sensitive materials and require appropriate drying before extrusion.
Recycled polymers can introduce additional contamination, viscosity variation, and wear considerations.
Therefore, “PET” or “nylon” alone is not always enough information for an accurate machine quotation.
2. Target Filament Diameter and Tolerance
The finished diameter is one of the most important inputs in monofilament equipment selection.
A 0.12 mm filtration filament and a 3 mm rope monofilament may require significantly different line configurations.
Define:
- Target diameter
- Minimum diameter
- Maximum diameter
- Diameter tolerance
- Ovality requirement
- Measurement method
Diameter tolerance is not the same as ovality
Diameter tolerance describes how much the filament diameter changes from the target value.
Ovality describes the difference between the filament’s major and minor dimensions across its cross-section.
For applications such as:
- Filter mesh
- Zipper monofilament
- Fine brush filament
- Fishing line
- Precision industrial filament
both parameters may be important.
A purchasing specification should therefore avoid simply stating:
Diameter: 0.20 mm ±0.01 mm
when roundness is also critical.
A better specification defines both the diameter acceptance range and ovality/roundness requirement, together with the measurement method.
3. Required Production Output
Output should be specified as:
kg/h at the target polymer, filament diameter, and production conditions.
Do not compare machines using only the maximum theoretical extruder capacity.
For example, a supplier may advertise a high output for a large extruder processing an easy-flowing polymer, but the stable production capacity may be substantially different when the machine is used for:
- Fine nylon filament
- High drawing ratios
- Recycled PET
- Tight diameter tolerances
- Multi-hole dies
Therefore, ask suppliers:
What stable output can this line achieve using my polymer and target filament diameter?
This is a much more useful purchasing question than:
What is the maximum output of the extruder?
4. End-Use Application
The final application determines the required downstream process.
Typical applications include:
- Brush filament
- Broom filament
- Toothbrush filament
- Zipper monofilament
- Fishing line
- Fishing net yarn
- Rope
- Agricultural mesh
- Filter mesh
- Synthetic grass
- Industrial technical filament
Different applications can require different combinations of:
- Drawing ratio
- Number of drawing stages
- Hot-water drawing
- Hot-air drawing
- Annealing
- Oil treatment
- Winding configuration
- Tension control
For example, a brush filament may require a different drawing and heat-setting process from a zipper monofilament.
Therefore, the end-use product should be defined before finalizing the line configuration.
5. Quality Acceptance Criteria
Machine specifications should be connected to measurable product requirements.
Before contacting suppliers, define the quality criteria that matter to your customers.
These may include:
- Diameter tolerance
- Ovality
- Tensile strength
- Elongation at break
- Stiffness
- Rebound
- Surface finish
- Color consistency
- Filament break rate
- Reject rate
These requirements can influence the selection of:
- Extruder temperature zones
- Melt filtration
- Die configuration
- Drawing stages
- Heat-setting system
- Online diameter measurement
- Winding tension control
A machine should ultimately be evaluated according to whether it can meet the required product specification, not simply whether its individual components look impressive on paper.
Key Monofilament Extrusion Machine Specifications
Once the production inputs are defined, the main equipment parameters can be evaluated.
The most important specifications include:
- Screw diameter
- Screw L/D ratio
- Screw geometry
- Screw and barrel material
- Temperature-zone configuration
- Motor and gearbox
- Melt filtration
- Melt pump
- Die/spinneret
- Downstream drawing
- Heat setting
- Winding
- Automation and quality monitoring
Screw Diameter: How Is the Correct Size Selected?
Screw diameter is one of the main factors determining extrusion capacity.
Industrial monofilament lines commonly use different screw diameters depending on:
- Required output
- Polymer
- Filament diameter
- Number of die holes
- Production speed
- Melt throughput
Smaller extruders may be suitable for lower-output or fine-filament applications, while larger extruders are used when higher throughput is required.
However, larger is not automatically better.
An oversized extruder may increase:
- Equipment cost
- Motor power
- Floor space
- Energy consumption
- Minimum economically efficient output
The correct screw diameter should therefore be calculated from the required production range.
Buyer question
Instead of asking:
“What is your largest extruder?”
ask:
“What screw diameter provides stable production at my required kg/h, polymer, and filament diameter?”
Screw L/D Ratio
The L/D ratio means the effective screw length divided by the screw diameter.
For example:
30:1 L/D = screw length approximately 30 times the screw diameter.
L/D influences the available space for:
- Solid conveying
- Polymer melting
- Mixing
- Homogenization
- Pressure development
For many industrial monofilament applications, an L/D in approximately the 28:1–33:1 range can be a useful engineering starting point.
A 30:1 configuration is commonly used for many PA, PET, and PP applications.
However, L/D should not be treated as a universal quality ranking.
A longer screw can provide more melting and homogenization length, but it can also increase residence time and thermal exposure.
Therefore:
L/D must be evaluated together with screw geometry, polymer characteristics, output, and thermal sensitivity.
Screw Geometry
Screw geometry can be more important than L/D alone.
Important parameters include:
- Compression ratio
- Feed-zone geometry
- Compression-zone length
- Metering-zone length
- Barrier section
- Mixing section
- Flight design
- Screw clearance
The purpose of the screw is to provide controlled:
Feeding → Melting → Homogenization → Metering
For demanding monofilament applications, an application-specific screw design may improve melt uniformity compared with a generic screw.
However, aggressive mixing is not automatically beneficial.
Excessive shear can increase melt temperature and may increase degradation risk for sensitive polymers.
The correct screw should therefore be designed around the specific resin and production conditions.
Temperature Zones and Melt Temperature Control
Temperature control is critical because polymer viscosity changes with temperature.
A temperature fluctuation can cause:
Temperature variation → Viscosity variation → Melt-flow variation → Diameter variation
For monofilament extrusion, several independently controlled barrel zones are typically used, together with adapter and die temperature control.
The exact number of zones depends on:
- Screw diameter
- L/D ratio
- Polymer
- Output
- Die configuration
- Required process control
For demanding applications, more independently controlled zones can provide finer control of the melting profile.
But the number of zones alone does not determine machine quality.
What should buyers verify?
Ask the supplier for:
- Number of independent zones
- Temperature-control method
- PID control
- Actual temperature stability
- Melt temperature measurement
- FAT temperature records
Most importantly:
Request actual production data rather than only temperature setpoints.
A machine displaying 270°C on the controller does not prove that the polymer melt is actually stable at that temperature during continuous production.
Die and Spinneret Design
The die or spinneret converts the polymer melt into continuous filaments.
Its design directly affects:
- Filament diameter
- Melt distribution
- Flow uniformity
- Die swell
- Surface quality
- Filament-to-filament consistency
Important specifications include:
- Number of holes
- Hole diameter
- Capillary geometry
- Land length
- Hole spacing
- Flow distribution
- Die temperature
For multi-hole monofilament production, uniform melt distribution across the die holes is especially important.
A die can be mechanically precise but still produce inconsistent filaments if melt distribution is uneven.
For applications requiring high roundness or dimensional stability, the spinneret should be designed according to the polymer’s melt-flow and die-swell characteristics.
Melt Filtration
Melt filtration removes contaminants and unmelted particles before the polymer reaches the die.
It is especially important when processing:
- Recycled PET
- Recycled PP
- Recycled PE
- Contaminated feedstock
- Fine monofilament
- Multi-hole spinnerets
Poor filtration can contribute to:
- Die blockage
- Filament breaks
- Surface defects
- Pressure fluctuations
- Uneven filament output
The filter should not be selected only by mesh number.
The supplier should consider:
Polymer + contamination level + output + filament diameter + acceptable pressure drop
For recycled material, filtration requirements can be significantly different from virgin resin production.
Should a Monofilament Extrusion Machine Use a Melt Pump?
A melt pump, also called a gear pump, is an optional component used to provide more controlled polymer melt delivery.
Its main purpose is to improve melt-flow consistency and reduce the influence of screw-output fluctuations.
A simplified configuration may be:
Extruder → Melt Filter → Melt Pump → Die
or another arrangement depending on the equipment design.
When is a melt pump useful?
A melt pump can be valuable when the production requires:
- Tight diameter control
- Stable melt flow
- Stable pressure at the die
- Fine technical filament
- High consistency across multiple die holes
Is a melt pump always necessary?
No.
For applications with less demanding dimensional requirements, a properly designed and tuned screw may provide sufficient melt stability.
A melt pump also adds:
- Equipment cost
- Maintenance requirements
- Seals
- Pressure requirements
- Another controlled component
Therefore, the decision should be based on the actual process requirement.
Important diagnostic principle
A melt pump can address melt-flow instability.
It cannot solve problems caused by:
- Unstable cooling water
- Uneven quenching
- Drawing roller speed variation
- Roller slip
- Incorrect draw ratio
- Winding tension instability
This distinction is extremely important when troubleshooting an existing monofilament line.
Downstream Drawing System
The extruder produces the initial filament, but the final filament properties are heavily influenced by the drawing process.
Drawing changes polymer molecular orientation and therefore affects:
- Tensile strength
- Elongation
- Stiffness
- Diameter
- Dimensional stability
A simplified production sequence is:
Extrusion → Quenching → Preheating → Drawing → Heat Setting → Winding
The number of drawing stages should be determined by the polymer and final product requirements.
One-Stage vs. Two-Stage Drawing
A one-stage drawing system can be suitable for some PP and PE applications.
A two-stage system provides additional control over deformation and molecular orientation and may be appropriate for demanding applications.
Depending on the polymer and product, drawing may use:
- Cold water
- Warm water
- Hot water
- Heated rollers
- Hot-air ovens
For brush and bristle applications, multi-stage drawing and controlled thermal treatment are commonly important for achieving the required combination of:
- Stiffness
- Strength
- Rebound
- Diameter consistency
The exact configuration should be determined through application testing rather than assuming one standard drawing system fits every filament.
Annealing and Heat Setting
After drawing, heat setting or annealing can help stabilize the filament.
The process can influence:
- Internal stress
- Dimensional stability
- Elongation
- Final mechanical properties
- Thermal stability
Depending on the polymer and application, heat setting can use:
- Hot-water systems
- Hot-air ovens
- Heated rollers
The correct process window depends on polymer type, draw ratio, filament diameter, and target properties.
Winding System
The winder is the final production module and should not be treated as an accessory.
The winding system must match the customer’s final package requirement.
Possible winding formats include:
- Bi-conical packages
- Flange spools
- Cross-wound bobbins
- Other application-specific packages
Important specifications include:
- Spindle count
- Maximum winding speed
- Tension control
- Package dimensions
- Automatic doffing
- Traverse system
A winder that cannot match the upstream production speed becomes a bottleneck.
Likewise, unstable winding tension can affect package quality and may introduce tension variation into the finished filament.
Material-Specific Monofilament Line Configuration
Different polymers require different equipment configurations.
The following table should be treated as an engineering reference rather than a universal process standard. Actual settings depend on resin grade, moisture level, output, filament diameter, screw design, and downstream process conditions.
Parameter | PA6 / PA66 | PET | PP | PE / HDPE |
Drying | Required | Required | Usually not required | Usually not required |
Typical thermal range | Polymer-grade dependent | Polymer-grade dependent | Polymer-grade dependent | Polymer-grade dependent |
Typical L/D starting point | ~30:1–33:1 | ~30:1–33:1 | ~28:1–30:1 | ~28:1–30:1 |
Screw/barrel consideration | Nitrided or wear-resistant design | Wear and degradation control | Nitrided commonly used | Nitrided commonly used |
Recycled-material sensitivity | Moisture / contamination / wear | Moisture / IV / contamination | Material-dependent | Material-dependent |
Drawing | Often multi-stage | Often multi-stage | One- or multi-stage | Application-dependent |
PET Monofilament: Why Extruder Selection Is Especially Important
PET monofilament extrusion requires careful control because PET is:
- Hygroscopic
- Sensitive to moisture during melt processing
- Sensitive to thermal history
- Sensitive to molecular-weight changes
For PET production, the extrusion system should therefore be evaluated together with:
Crystallization → Drying → Extrusion → Filtration → Drawing → Heat Setting
When using recycled PET, additional attention should be given to:
- Feedstock quality
- Contamination
- Melt filtration
- Intrinsic viscosity
- Thermal history
- Screw and barrel wear
A PET machine quotation that only specifies the extruder but does not clearly define the drying and filtration system is incomplete for many industrial applications.
PA6 and PA66 Monofilament: Moisture Control
PA6 and PA66 absorb moisture from the environment.
If the resin is not properly dried before extrusion, production problems may include:
- Bubbles
- Surface defects
- Reduced mechanical performance
- Hydrolysis
- Unstable drawing
Therefore, a nylon monofilament line should be evaluated as:
Drying System + Extruder + Filtration + Die + Drawing + Heat Setting
rather than treating the extruder as an isolated machine.
Automation and Process Monitoring
A monofilament line should not only produce good filament during the initial commissioning test.
It should also maintain stable production across:
- Different shifts
- Material batches
- Long production runs
- Startup and shutdown
- Material changes
Important control functions can include:
- Zone-by-zone temperature monitoring
- Screw-speed control
- Melt-pressure monitoring
- Motor-load monitoring
- Drawing-speed synchronization
- Winder-speed control
- Alarm management
- Production data logging
- Online diameter measurement
Online Diameter Measurement
For applications with tight dimensional requirements, an online laser or optical diameter gauge can provide continuous monitoring.
The system can detect:
- Diameter drift
- Sudden diameter changes
- Process instability
- Out-of-spec production
A more advanced configuration can connect the measurement system to process controls for feedback or alarm functions.
The key advantage is that problems can be detected during production rather than after an entire batch has been manufactured.
PLC and Control-System Considerations
The PLC and control architecture affect long-term serviceability.
When purchasing equipment for an overseas factory, buyers should consider:
- PLC manufacturer
- HMI availability
- Spare hardware
- Software backup
- Parameter backup
- Remote technical support
- Alarm history
- Data logging
Common industrial automation platforms may offer easier international maintenance, but the most important issue is not the brand alone.
The buyer should confirm that the supplier can provide:
Documentation + Backup + Technical Support + Replacement Parts
Factory Acceptance Test: What Should You Verify?
A Factory Acceptance Test (FAT) should verify actual production performance before shipment.
The FAT should be based on the agreed product specification.
Important items include:
Extrusion
- Polymer used
- Screw speed
- Output kg/h
- Motor load
- Melt pressure
- Melt temperature
Temperature
- Barrel-zone temperatures
- Adapter temperature
- Die temperature
- Temperature stability during continuous operation
Filament
- Diameter
- Diameter variation
- Ovality where applicable
- Surface quality
- Filament break rate
- Tensile properties where agreed
Downstream
- Drawing ratio
- Roller synchronization
- Heat-setting temperature
- Winding speed
- Winding tension
- Package quality
Documentation
- FAT report
- Electrical documentation
- Mechanical drawings where applicable
- Spare-parts list
- Operation manual
- Maintenance instructions
The FAT should use conditions that are representative of the buyer’s actual production requirements whenever practical.
How to Evaluate a Monofilament Machine Supplier
Machine specifications alone do not prove machine performance.
A supplier should be evaluated in four areas:
1. Technical Capability
Can the supplier explain why the proposed:
- Screw diameter
- L/D ratio
- Screw geometry
- Die
- Drawing system
- Winder
matches your application?
2. Application Experience
Ask for references involving:
- The same polymer
- Similar filament diameter
- Similar output
- Similar application
A supplier experienced in heavy PP monofilament may not automatically have the same expertise in fine PET or nylon filament.
3. FAT Capability
Ask:
Can you run my material and target filament before shipment?
The stronger answer is supported by documented FAT criteria and actual production data.
4. After-Sales Support
Ask about:
- Installation
- Commissioning
- Operator training
- Remote technical support
- Spare parts
- Software support
- Troubleshooting
- Engineer service
After-sales capability should be treated as part of the machine specification because production downtime has a direct financial cost.
Questions to Ask Before Buying a Monofilament Extrusion Machine
Use these questions when comparing suppliers.
Question 1
What screw diameter do you recommend for my required kg/h and filament diameter?
The answer should be based on your actual production conditions.
Question 2
What L/D ratio and screw geometry are proposed, and why?
The supplier should explain the relationship between the screw design and your polymer.
Question 3
What output can the machine maintain continuously at my target diameter?
Do not accept only a theoretical maximum output.
Question 4
What temperature stability can you demonstrate during FAT?
Ask for actual process records where possible.
Question 5
What melt filtration system is included?
Especially important for recycled polymers and fine filament.
Question 6
Is a melt pump necessary for my product?
The supplier should explain the process reason.
Question 7
How is the final filament diameter measured?
Ask whether measurement is:
- Offline
- Online
- Single-axis
- Dual-axis
and what sampling method is used.
Question 8
What drawing and heat-setting configuration is recommended?
This should be based on the final filament properties.
Question 9
What FAT criteria are included in the purchase contract?
The FAT should be measurable and documented.
Question 10
What spare parts and technical support are included?
Clarify lead times before placing the order.
Red Flags When Comparing Suppliers
Pay additional attention when a supplier provides:
1. Output numbers without conditions
For example:
“Output: 120 kg/h”
without specifying:
- Polymer
- Filament diameter
- Die configuration
- Production conditions
is not enough information for comparison.
2. L/D ratio without explanation
A number such as 30:1 has little meaning without knowing why it was selected.
3. No application references
A supplier should be able to demonstrate relevant experience.
4. No documented FAT
If performance cannot be tested and documented before shipment, the buyer carries greater commissioning risk.
5. Certifications without documentation
Ask for the relevant certification or declaration documents.
6. Extremely low quotation without technical explanation
A low price may result from differences in:
- Screw material
- Barrel construction
- Motor
- Gearbox
- Temperature control
- Filtration
- Automation
- Drawing equipment
- Winder
- FAT scope
- After-sales service
Price should therefore be compared against the complete technical specification, not the machine name.
Monofilament Extrusion Machine Selection Checklist
Use this checklist before requesting a quotation.
Selection Area | What the Buyer Should Define | What the Supplier Should Confirm |
Polymer | Resin family and grade | Screw and process configuration |
Resin condition | Virgin / recycled / blend | Drying and filtration |
Diameter | Target and range | Die and drawing configuration |
Tolerance | Diameter and ovality | Measurement method |
Output | kg/h at target product | Stable production capacity |
Application | Final product | Complete downstream configuration |
Screw | Diameter and L/D | Application-specific design |
Temperature | Process window | Independent control zones |
Filtration | Contamination level | Filter configuration |
Melt pump | Required or optional | Technical justification |
Drawing | Product requirements | One- or multi-stage system |
Annealing | Mechanical requirements | Hot-water or hot-air system |
Winding | Package format | Winder type and tension control |
Automation | Monitoring requirements | PLC/HMI/data functions |
FAT | Acceptance criteria | Test report |
Certification | Import/customer requirements | Documentation |
Support | Installation and training | Service scope |
Spare parts | Critical components | Lead time and availability |
How to Compare Two Monofilament Extrusion Machines
When two suppliers offer different machines, compare them using the same technical conditions.
Parameter | Supplier A | Supplier B |
Polymer | ||
Resin condition | ||
Screw diameter | ||
L/D ratio | ||
Screw geometry | ||
Screw material | ||
Barrel material | ||
Heating zones | ||
Motor power | ||
Gearbox | ||
Melt filtration | ||
Melt pump | ||
Die hole count | ||
Target output | ||
Stable output | ||
Drawing stages | ||
Annealing | ||
Online diameter gauge | ||
Winder | ||
FAT | ||
Warranty | ||
Spare-parts support |
This comparison prevents a common procurement mistake:
comparing two machines by price before confirming that they are actually configured for the same production requirements.
What Information Does a Supplier Need to Design the Line?
A supplier can usually prepare a much more meaningful preliminary configuration when the buyer provides at least four core inputs:
1. Polymer
Example:
PA6 / PA66 / PET / PP / PE / HDPE
2. Finished Diameter
Example:
0.20–0.30 mm
3. Production Output
Example:
50 kg/h
4. End-Use Product
Example:
filter mesh monofilament / brush filament / zipper monofilament / fishing line
Additional information such as recycled content, diameter tolerance, tensile strength, elongation, winding format, and production schedule will further improve the accuracy of the proposal.
From Product Specification to Machine Configuration
The most reliable selection logic is:
Final Product
↓
Polymer + Resin Condition
↓
Diameter + Tolerance
↓
Required Output
↓
Die / Spinneret
↓
Extruder Screw Diameter
↓
Screw Geometry + L/D
↓
Temperature-Control System
↓
Filtration + Melt Pump
↓
Quenching
↓
Drawing
↓
Heat Setting
↓
Winding
This sequence explains why a monofilament extrusion machine should not be selected simply from a catalogue.
The complete line must be designed around the final product specification.
Frequently Asked Questions
What is a monofilament extrusion machine?
A monofilament extrusion machine is equipment used to melt thermoplastic polymer and continuously form it into monofilament through a die or spinneret. A complete line also includes quenching, drawing, heat setting, and winding equipment.
What polymers can be processed on a monofilament extrusion line?
Common materials include PA6, PA66, PET, PP, PE, HDPE, PBT, and selected polymer blends. The screw, temperature profile, drying, filtration, die, and drawing configuration should be matched to the specific material.
What screw L/D ratio is suitable for monofilament extrusion?
Many industrial applications use an L/D in approximately the 28:1–33:1 range. Around 30:1 is a common starting point, but the appropriate L/D depends on polymer, output, screw geometry, and thermal requirements.
Is a bigger extruder always better?
No. An oversized extruder can increase capital cost, motor power, floor space, and operating cost. The correct extruder should provide stable output within the required production range.
Does the extruder determine the final filament diameter?
No. The final diameter depends on the interaction between extrusion output, die geometry, quenching, drawing ratio, drawing speed, heat setting, and winding conditions.
Is a melt pump necessary for monofilament production?
Not always. A melt pump can improve melt-flow stability for demanding applications, but it is not a universal requirement. The decision should be based on diameter tolerance, output stability, die configuration, and process requirements.
Why is drying important for PET and nylon?
PET, PA6, and PA66 are moisture-sensitive polymers. Insufficient drying can contribute to hydrolysis, bubbles, surface defects, reduced mechanical performance, and unstable processing.
What should be included in a monofilament machine FAT?
A FAT should define measurable criteria for extrusion output, temperature stability, melt pressure, filament diameter, relevant mechanical properties, drawing behavior, winding performance, alarms, and other agreed machine functions.
How do I compare monofilament extrusion machine suppliers?
Compare suppliers using the same polymer, diameter, output, application, FAT conditions, machine configuration, warranty, spare-parts support, and technical service requirements. Do not compare only the machine price or maximum output.
Can one monofilament extrusion machine produce different products?
A line may be designed to process different materials or products, but changing polymer, diameter, or application can require different process parameters, dies, drawing conditions, and winding configurations. The supplier should confirm the actual material and product range supported by the proposed line.
Conclusion: Choose the Complete Process, Not Just the Extruder
The most important principle when buying a monofilament extrusion machine is simple:
The correct machine is the one that matches the polymer, filament specification, production output, and end-use application under real operating conditions.
A reliable monofilament line connects:
Material Preparation → Extrusion → Filtration → Die → Quenching → Drawing → Heat Setting → Winding
Every stage affects the final product.
The extruder determines the quality and stability of the polymer melt. The die determines melt distribution. The quenching system controls initial filament solidification. The drawing system establishes molecular orientation and final dimensions. Heat setting stabilizes the filament, while the winder determines package quality and production continuity.
Therefore, the best purchasing decision is not:
“Which supplier offers the biggest extruder?”
It is:
“Which supplier can demonstrate that the complete line will produce my required filament specification at stable production output?”
About NLY Monofilament Extrusion Solutions
Changzhou Xinliaoyuan Machinery Co., Ltd. (NLY) has manufactured monofilament extrusion equipment since 1989 and supplies complete monofilament production solutions for different polymer and application requirements.
NLY’s equipment solutions cover applications including:
- PA and nylon monofilament
- PET monofilament
- PP monofilament
- PE/HDPE monofilament
- Brush and broom filament
- Zipper monofilament
- Fishing line and fishing net filament
- Rope monofilament
- Industrial mesh and filtration filament
- Other specialty monofilament applications
For a project-specific proposal, the most useful starting information is:
Polymer + Target Diameter + Required Output + End-Use Application
Additional information about recycled content, diameter tolerance, mechanical requirements, and winding format can be used to refine the configuration.
NLY can then evaluate the appropriate extruder size, L/D ratio, screw configuration, die, drawing system, heat-setting system, winding system, and auxiliary equipment according to the production requirements.







