
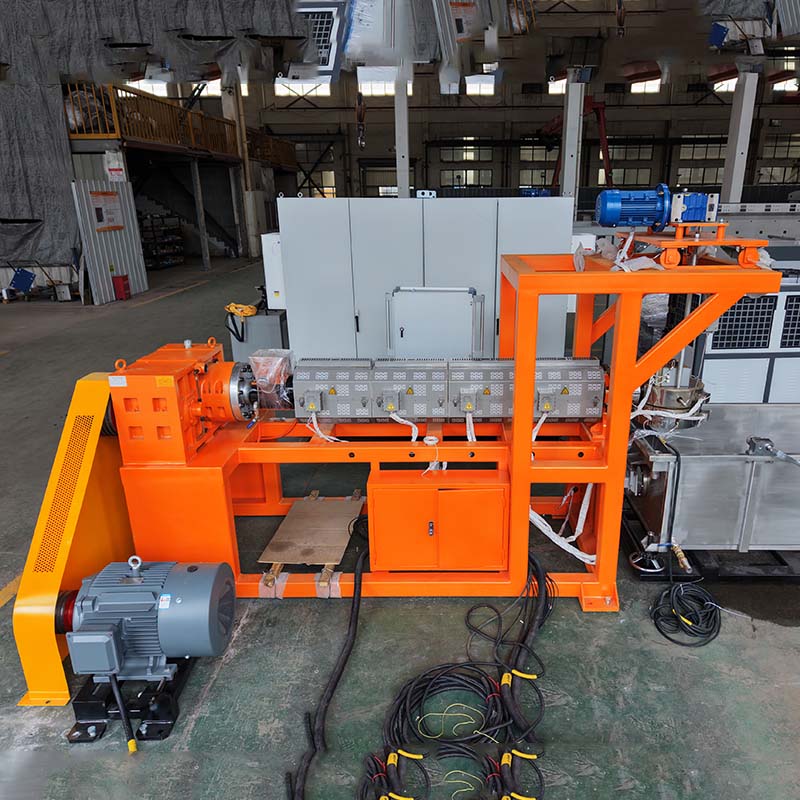
Manufacturing high-performance synthetic brush bristles requires uncompromising extrusion consistency. Whether producing fine tapered PBT bristles for cosmetic brushes, durable PET filaments for street sweepers, flaggable PP broom fibers, or abrasive nylon monofilaments for industrial deburring, the quality of the end product depends on the precise engineering of your brush filament extrusion machine.
A minor fluctuation in melt pressure, temperature drift in the quenching trough, or uneven draw ratios across the roller stand leads to severe production defects—such as diameter variations, ovality, bristle curl memory loss, and frequent line breaks.
This technical buyer’s guide breaks down the core line engineering, polymer-specific processing parameters, component selection criteria, and operational evaluation frameworks needed to configure a reliable, high-yield synthetic brush bristle production line.
Understanding the Brush Filament Extrusion Process: From Polymer to Precision Bristles
A complete brush filament extrusion line transforms raw thermoplastic resin pellets or washed recycled bottle flakes into continuous, highly oriented monofilament strands with tightly controlled mechanical and physical properties. Achieving high tensile strength, consistent flexural recovery, and uniform diameter across hundreds of simultaneous strands requires a synchronized multi-stage manufacturing system.
Polymer Dryer & Hopper → Single-Screw Extruder → Melt Metering Pump → Spinneret Die → Quenching Tank → Primary Draw Stand → Hot Water/Air Heating Oven → Secondary Draw Stand → Heat-Setting Annealing Oven → Oiling & Waving Unit → Automatic Spool Winder / Bundle Cutter
1. Single-Screw Plasticization & Melt Metering Control
The plasticization stage begins with feeding pre-dried polymer chips into the single-screw extruder barrel. The primary objective is to achieve a completely homogeneous polymer melt free from thermal degradation or un-melted gels.
Screw Geometry: Monofilament lines typically employ single screws with a length-to-diameter (L/D) ratio between 30:1 and 32:1. Deep-flight feeding zones, barrier compression sections, and high-shear mixing heads ensure uniform plasticization.
Gear Metering Pumps: Positioned between the extruder barrel and die head, precision gear pumps maintain volumetric output stability. By buffering pressure surges from the screw flights, metering pumps keep melt pressure variations at the die face below ±0.5 bar, preventing filament pulsing and denier drift.
Spinneret Distribution: The molten polymer passes through multi-layer screen changers before entering the spinneret die head. Spinneret plates contain hundreds of micro-drilled capillary orifices arranged in optimized pattern layouts to prevent filament merging and ensure balanced melt velocity across every individual strand.
Key Takeaway: A precision gear metering pump is mandatory for brush monofilament extrusion. Relying solely on extruder screw pressure creates melt surging, resulting in unacceptable filament diameter tolerances.
2. Quenching, Multi-Stage Orientation, and Heat Setting
Once extruded from the spinneret, molten polymer strands enter the downstream cooling and orientation assembly:
Water Quenching: The molten strands fall into a temperature-controlled stainless steel water bath (typically maintained between 15°C and 25°C). Rapid cooling freezes the polymer into an amorphous state before crystallization occurs, making the filaments pliable for subsequent stretching.
Multi-Stage Tensile Drawing: Filaments pass through primary Godet roller stands and enter a hot water bath or hot air draw oven. Subjecting the filaments to stretch ratios between 3.5:1 and 6.0:1 aligns chaotic polymer chains along the longitudinal axis, dramatically increasing tensile tenacity and flexural modulus.
Heat-Setting Annealing: High draw ratios induce internal molecular stresses. Passing drawn filaments through a multi-zone hot air annealing oven (140°C to 180°C) with controlled relaxation rollers relieves residual stress. This thermal stabilization prevents post-production shrinkage, warping, and bristle curl memory loss when exposed to hot water or cleaning solvents.
Surface Finishing & Winding: Filaments receive an anti-static oil bath coating to improve tufting machine feeding. For broom bristles, inline crimping rollers introduce a wavy profile before the strands are wound onto spools or automatically cut into fixed bundle lengths.
Polymer-Specific Processing Matrix: PET, PBT, Nylon (PA6/PA66), and PP
Different brush applications require distinct polymer chemistries. Choosing the correct machinery configuration depends on understanding how each polymer behaves during melting, quenching, drawing, and crystallization.
Processing Parameter | PET (Polyester) | PBT (Polybutylene) | PA6 / PA66 (Nylon) | PP (Polypropylene) |
|---|---|---|---|---|
Drying Target | ≤ 0.005% (50 ppm) | ≤ 0.03% (300 ppm) | ≤ 0.02% (200 ppm) | Non-hygroscopic (Standard dry) |
Drying Condition | 150°C–170°C (4–6 hrs) | 110°C–120°C (3–4 hrs) | 80°C–90°C (4–6 hrs) | Pre-heating optional |
Melt Temperature | 260°C – 290°C | 230°C – 260°C | 230°C – 285°C | 200°C – 240°C |
Quenching Temp | 18°C – 25°C | 20°C – 30°C | 15°C – 20°C | 20°C – 35°C |
Stretch Draw Ratio | 4.0:1 – 5.5:1 | 3.5:1 – 4.5:1 | 3.5:1 – 5.0:1 | 4.0:1 – 6.0:1 |
Annealing Temp | 160°C – 180°C | 140°C – 160°C | 150°C – 170°C | 100°C – 120°C |
Primary End Use | Brooms, street sweepers | Toothbrushes, paint brushes | Industrial & abrasive brushes | Household brooms & ropes |
PET Brush Filament Extrusion: Dehumidifying Drying & High Tenacity
PET (Polyester) is widely used for household broom bristles, industrial brushes, and outdoor sweeping brooms due to its high tensile strength, stiffness, and cost-effectiveness when processing recycled bottle flakes.
Moisture Control: PET is extremely sensitive to hydrolytic degradation at elevated melt temperatures. Moisture levels above 50 ppm cause rapid intrinsic viscosity (IV) drop, resulting in brittle filaments that break during drawing. A closed-loop desiccant dehumidifying drying system with a dew point below -40°C is essential.
Process Dynamics: Requires a multi-zone hot air draw oven and high-temperature heat setting (160°C–180°C) to lock in vertical straightness and eliminate thermal shrinkage during shipping or storage.
PBT Brush Filament Extrusion: Superior Wet Bend Recovery
PBT is the preferred resin for premium paint brushes, cosmetic brushes, and toothbrushes. PBT filaments offer exceptional wet bend recovery, abrasion resistance, and chemical durability.
Processing Requirements: PBT exhibits faster crystallization kinetics than PET. Precise water bath quenching distance and temperature management are critical to prevent premature crystallization before primary drawing.
Secondary Processing: PBT filaments are frequently chemically tapered using caustic baths or mechanical flagging. Monofilament extruders dedicated to PBT must maintain tight wall thickness tolerances to ensure uniform chemical etching rates. Manufacturers producing specialized brush bristles often configure dedicated PBT and abrasive nylon monofilament extrusion lines to handle delicate chemical and mechanical post-treatments.
Nylon (PA6/PA66) Abrasive & High-Wear Industrial Bristles
Nylon monofilaments provide unmatched flex fatigue resistance, toughness, and thermal resistance for heavy-duty industrial polishing, car wash brushes, and abrasive grit bristles filled with silicon carbide or aluminum oxide.
Wear Resistance: Processing abrasive-filled PA6/PA66 resins accelerates barrel and screw wear. Extruders must feature bimetallic barrels with tungsten carbide liners and fully armor-plated screw flights to ensure long service life.
Moisture Management: Nylon is highly hygroscopic and requires low-temperature vacuum drying to avoid discoloration and bubble formation.
Polypropylene (PP) Utility & Household Broom Bristle Lines
Polypropylene represents an economical choice for utility broom bristles, street sweeping fibers, and agricultural brushes.
Processing Advantages: PP is non-hygroscopic and requires minimal drying energy. It yields lightweight filaments with excellent chemical resistance.
Orientation Control: PP exhibits significant elastic memory. High draw ratios (up to 6.0:1) combined with inline waving/crimping units produce soft-flagged broom bristles with superior dust-collecting capability. Factories focusing on high-volume cleaning products often utilize specialized PP brush bristle extruding equipment configured for rapid line speeds and inline crimping.
Pro Tip: When switching between PET and Nylon production on a single extrusion line, purge the barrel thoroughly with a high-viscosity purging compound and recalibrate quench bath distances. Nylon requires lower water quenching temperatures and longer immersion times than PET to prevent internal voids.
Critical Machinery Line Selection Criteria for Synthetic Brush Bristle Production
Selecting the right monofilament brush bristle extruder involves evaluating core line hardware, drive automation, temperature stability, and auxiliary integration.
1. Screw L/D Ratio and Drive Automation
The single-screw extruder serves as the heart of the extrusion line:
Screw Design (30:1 / 32:1 L/D): Extended L/D ratios provide adequate residence time for complete plasticization without overheating the polymer melt. Nitrogen-treated nitrided steel (38CrMoAlA) or bimetallic alloy construction resists corrosion and abrasive wear.
Drive Motors & Inverters: Variable frequency drives (VFD) from Siemens or ABB coupled with heavy-duty helical gear reducers ensure precise screw speed regulation from 0 to 80 RPM with minimal torque ripple.
Heating Control: Cast-aluminum heaters with multi-zone PID temperature controllers (such as Omron) maintain barrel temperature accuracy within ±1°C across all heating zones.
2. Melt Metering Gear Pumps and Diameter Tolerance Management
Achieving tight filament diameter tolerances (±0.002 mm for fine toothbrush bristles; ±0.005 mm for heavy broom fibers) requires active melt flow management.
Melt Pump Integration: High-precision gear pumps driven by independent servo motors maintain constant volumetric feeding to the die head regardless of screw pressure changes.
Laser Diameter Gauges: Non-contact dual-axis laser measuring heads positioned after the primary draw stand continuously monitor filament denier. Closed-loop feedback systems automatically adjust Godet roller draw speeds to correct diameter deviations in real time.
3. Multi-Stage Drawing Units and Heat-Setting Annealing Ovens
Stretching and thermal stabilization determine the structural integrity of the finished bristle.
Godet Rollers: Chrome-plated, mirror-polished Godet rollers driven by individual AC servo drives allow fine-tuning of draw ratios across primary and secondary stretch zones.
Heating Ovens: Hot water stainless steel troughs or circulating hot-air drying ovens provide uniform heat transfer across the entire filament sheet. For detailed orientation mechanics, plant engineers can review our engineering guide on the multi-stage monofilament stretching and drawing process.
Annealing Stabilization: Thermal heat setting prevents bristle bending or curling during long-term storage or high-speed tufting machine operations.
Technical Evaluation Checklist for Monofilament Line Buyers
Before purchasing a synthetic brush bristle production line, production managers and engineering directors should conduct a systematic evaluation using the following criteria:
Evaluation Criteria | Benchmark / Specification | Target Plant Floor Objective |
|---|---|---|
Screw L/D & Metallurgy | 30:1 or 32:1 L/D ratio; Bimetallic alloy barrel | Complete plasticization; 5+ years screw lifespan under filled resins |
Melt Flow Stability | Melt gear pump with pressure fluctuation < ±0.5 bar | Uniform volumetric output; zero filament diameter surging |
Diameter Tolerance | Dual-axis laser closed-loop control (±0.002 to ±0.005 mm) | Minimal scrap rates; high-speed tufting compatibility |
Energy Consumption | Specific power consumption ≤ 0.35–0.45 kWh/kg | Reduced operating costs; improved ROI |
Temperature Control | Multi-zone PID control (±1°C accuracy) | Prevents thermal degradation and intrinsic viscosity (IV) drop |
Drying System | Desiccant dehumidifying dryer (Dew point ≤ -40°C) | Hydrolysis prevention for PET/Nylon processing |
Line Speed & Output | 80 to 200 kg/h throughput (model dependent) | Maximized Overall Equipment Effectiveness (OEE) |
Certifications & Spares | ISO 9001:2008 & CE certified; standard electrical parts | Compliance verification; minimal Mean Time to Repair (MTTR) |
Factories planning new line installations or upgrading existing capacities can explore customized broom and brush filament extrusion solutions tailored to specific factory layouts, output targets, and raw material selections.
Troubleshooting Common Brush Monofilament Extrusion Defect Modes
Even on well-engineered lines, operational variables can introduce defect modes. The following table highlights common processing challenges and immediate corrective actions:
Defect / Failure Mode | Root Cause Analysis | Plant-Floor Corrective Action |
|---|---|---|
Frequent Line Breaks during Drawing | High moisture content in PET/Nylon; un-melted gels; uneven quenching bath temperature | Verify dryer dew point (≤ -40°C); increase barrel zone 2–3 heat; lower quench bath temp |
Filament Ovality / Non-Roundness | Uneven cooling rate in water trough; excessive die swell | Adjust quench water air-knife wiper pressure; calibrate die orifice land length |
Bristle Curl Memory Loss / Warping | Insufficient heat-setting annealing temperature or time | Increase annealing oven temp (150°C–170°C); adjust relaxation Godet speed ratio |
Diameter Surging / Denier Fluctuation | Extruder screw surging; worn melt pump gears; temperature drift | Check gear pump drive speed stability; clean screen changers; calibrate PID zones |
For a complete diagnostic workflow covering mechanical, thermal, and material factors, plant operators can refer to our monofilament extrusion troubleshooting guide.
Frequently Asked Questions (FAQ)
What is the typical output capacity of a brush filament extrusion line?
Output capacities vary based on screw diameter and target filament thickness. Compact lines utilizing 65 mm screws produce 35 to 50 kg/h, while larger commercial monofilament extrusion lines equipped with 90 mm or 110 mm screws generate 120 to 200 kg/h for heavy PET or PP broom fibers.
Can a single extrusion machine process PET, PBT, and Nylon on the same line?
Yes, multi-purpose monofilament lines can process PET, PBT, and PA6/PA66. However, processing requirements differ: PET requires high-temperature desiccant drying (160°C), Nylon requires low-temperature vacuum drying, and PBT demands precise quenching bath distances. Operators must adjust barrel heating zones, drying equipment, and quench trough parameters when switching polymers. For further material comparison insights, review our guide on selecting polymers for monofilament production.
How do I prevent bristle bending or curling during tufting?
Bristle curling occurs when internal molecular stresses are not fully relaxed during production. Ensuring a robust heat-setting annealing stage (using multi-zone hot-air ovens at 140°C–180°C with relaxation Godet rollers) permanently stabilizes the molecular orientation, providing straight bristles with high bend recovery.
What is the advantage of using recycled PET bottle flakes for broom bristle production?
Recycled PET bottle flakes significantly reduce raw material costs while maintaining excellent tensile strength and stiffness. However, washed rPET flakes require efficient melt filtration screen changers and high-vacuum degassing extruders to remove volatile impurities and moisture before spinning.
Partner with NLY Machinery for Your Brush Extrusion Lines
Since 1989, Changzhou New Liaoyuan Machinery Co., Ltd. (NLY) has specialized in manufacturing complete monofilament extrusion lines for partners across more than 20 countries. Operating under ISO 9001:2008 and CE certified quality systems, NLY provides custom-engineered single-screw extruders, high-precision draw stands, and energy-efficient annealing systems designed for maximum uptime and long-term production efficiency.
Whether you are establishing a new synthetic brush bristle manufacturing plant or upgrading existing line capacity, NLY offers comprehensive turnkey support—including custom screw design, factory installation, operator training, and trial filament sampling.
Need a custom machinery specification or trial filament test plan?
Contact the NLY engineering team today to receive a tailored line layout, energy consumption calculation, and machinery quotation for your production requirements.







