
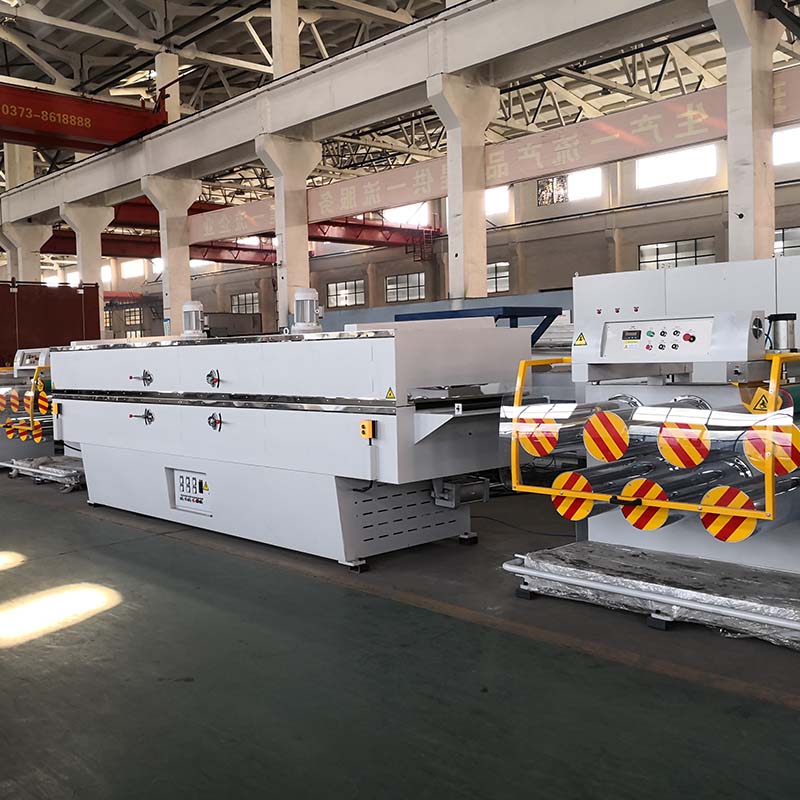
Nylon brush filaments are the backbone of modern brush manufacturing. From oral-care toothbrushes and cosmetic applicators to industrial abrasive rollers, street-sweeping brooms, and cleaning tools, polyamide bristles deliver the bend recovery, abrasion resistance, and dimensional stability that natural animal bristles cannot. But producing these filaments at commercial scale is not a matter of buying a generic plastics extruder and turning it on.
A nylon brush filament extrusion machine is a purpose-built, multi-stage thermo-mechanical line. It must dry a hygroscopic resin to a fraction of a percent moisture, melt it at sharp, grade-specific temperature windows, meter it surge-free, orient it through controlled drawing, stabilize it with heat setting, and wind it onto spools without introducing diameter drift. Get one of those stages wrong and the finished bristle shows up as bubbles, ovality, breakage, or lost curl memory on the brush plant floor.
This guide is written for plant managers, process engineers, operations directors, and purchasing leads evaluating a nylon brush filament extrusion line. It walks through what to specify stage by stage, the PA6/PA66/PA612 differences that change your machinery choices, and the red flags to catch before you commit capital.
Start With a Needs Assessment, Not a Machine Catalog
Before comparing vendor quotes, define the operating point your line must hit. A machine sized for industrial sweeping brooms will be badly misconfigured for fine cosmetic bristles, and vice versa. Lock down four inputs:
Target filament diameter and tolerance. Fine toothbrush and cosmetic bristles (0.05–0.25 mm) demand fine spinneret orifices, tighter draw control, and closed-loop laser gauging. Heavy sweeping or industrial brushes (0.5–3.0 mm) need larger screw capacity and robust winders.
Throughput. Decide kg/h or kg/24h at the operating diameter. Screw size and heating capacity scale directly with output.
Resin grade. PA6, PA66, or PA612 each impose different temperature zones, drying requirements, and draw-ratio limits (detailed below).
Downstream finish. Do you need crimped/curled bristles, tapered filaments, flagging, or antistatic oiling? Each affects which stations the line must include.
Key Takeaway: Write down your target diameter, tolerance, throughput, and grade before you look at any supplier. The machinery that fits a coarse sweeping-broom line is not the machinery that fits a fine toothbrush line.
Choosing the Right Nylon Grade Changes Your Line Specs
Polyamide is not one polymer. The three grades you will most often process for brush filaments behave differently enough to change drying, heating, and drawing requirements on the machine. A useful starting summary:
Resin Grade | Moisture Absorption | Melting Point | Bend Recovery | Typical Brush Applications |
|---|---|---|---|---|
PA6 | High (2.8–3.2%) | 220–225°C | Good | General cleaning brushes, brooms, commercial scrubbers |
PA66 | Moderate (2.5–2.8%) | 255–265°C | Excellent | High-speed industrial brushes, abrasive tools, automotive wash rollers |
PA612 | Low (~1.0–1.3%) | 212–220°C | Premium | Toothbrushes, cosmetic brushes, wet-environment technical brushes |
Bend-recovery differences between grades are well documented in industry reference data such as the Monahan Filaments technical bulletins, which publish measured recovery and ovality values across bristle diameters — a useful benchmark to carry into your own acceptance testing.
Because nylon is strongly hygroscopic, the line’s drying station is non-negotiable regardless of grade. If the resin enters the barrel with absorbed moisture, water vaporizes at melt temperature and causes hydrolytic degradation, micro-porosity, melt surging, and strand breakage. In practice this means a closed-loop desiccant dryer capable of a dew point of −40°C, taking the resin below 0.05% moisture — and to 0.02–0.03% for PA66 and PA612, which are run at higher draw ratios.
⚠️ Warning: Do not treat an oven or hopper dryer as a substitute for a closed-loop desiccant system on nylon. Undried polyamide is the single most common cause of bubbles, die drool, and breakage on a brush filament line.
Core Line Architecture of a Nylon Brush Filament Extrusion Machine
A complete line operates as a coordinated sequence. Each stage sets up the next, so the full configuration matters more than any single component.
Resin Drying → Extrusion & Melt Metering → Spinneret Die → Water Quench → First Draw → Second Draw (hot air/water) → Heat-Setting Annealing → Crimping & Oiling → Automatic Winding
For a full picture of how this configuration is sized and specified for polyamide bristles, this nylon bristle extrusion line configuration guide walks through component sizing in detail.
1. Closed-Loop Desiccant Drying Station
Because every nylon grade is hygroscopic, the line must begin with aggressive drying. Specify a desiccant dryer delivering air at a dew point of −40°C and holding the resin below 0.05% moisture before it reaches the hopper. This single station prevents the majority of moisture-driven defects: bubbles, porosity, melt surging, and brittleness in the drawn filament.
2. Single-Screw Extruder With a Barrier Screw
The extruder melts and homogenizes the polymer, but nylon’s sharp melting point and low melt viscosity punish sloppy thermal control. A nylon-capable line uses a single-screw extruder with a 30:1 L/D ratio and barrier screw geometry to plasticize uniformly without overheating. The barrel and screw metallurgy matter: bimetallic barrels and hardened flights extend service life because nylon is processed hot and can be abrasive over continuous runs.
3. Gear Melt Pump for Surge-Free Metering
Nylon’s low melt viscosity means screw pulsation translates directly into diameter fluctuation. A positive-displacement gear melt pump between the barrel and die isolates flow from screw surging, so volumetric output to the spinneret stays constant. This is one of the clearest technical deal-breakers to check for on any quote.
4. Spinneret Die and Water Quench
The spinneret plate contains the micro-drilled orifices that define filament diameter and cross-section. Freshly extruded strands then freeze in a temperature-controlled water quench bath (generally 15–20°C for nylon), which sets the amorphous structure needed for drawing. Quench temperature stability within a degree or two is critical — swings cause ovality and inconsistent crystallization.
5. Multi-Stage Hot Drawing and Orientation
Undrawn nylon strands have low tensile strength and no bend recovery. The draw section stretches the filament along its molecular axis to orient the polymer chains. Industrial lines use multi-stage drawing — a first draw in a hot water bath (about 80–95°C) followed by a hot-air oven draw where needed — to reach the target orientation without over-straining. Draw-ratio control between synchronized godets is what holds diameter and cross-section stable.
6. Heat-Setting Annealing
After drawing, the filament carries internal stress that would otherwise cause shrinkage and lost curl memory in the finished brush. A heat-setting annealing oven relaxes the structure and locks in dimensional stability and resilience. For PA6 and PA66 this typically runs around 170–200°C.
Stage-by-stage, these are the stations a complete line needs. For a deeper look at how each element of the production sequence connects end to end, see how a monofilament extrusion line operates for brush bristle filament.
Grade-Specific Processing Windows to Specify
Different grades need different barrel profiles, draw ratios, and annealing conditions. When you receive a quote, confirm the machine is configured for the grade you intend to run — a line set up for PA66 will overheat PA612 and under-orient PA6.
Parameter | PA6 | PA66 | PA612 |
|---|---|---|---|
Feed zone temperature | 220–230°C | 250–260°C | 215–225°C |
Transition zone temperature | 235–245°C | 265–275°C | 225–235°C |
Metering zone temperature | 245–255°C | 275–290°C | 235–245°C |
Die / melt temperature | 245–250°C | 270–280°C | 235–240°C |
Typical total draw ratio | 4.2–4.8:1 | 4.5–5.2:1 | 3.5–4.5:1 |
Heat-setting anneal | 170–200°C | 170–200°C | 140–180°C |
Across grades, the overall total draw ratio for good bend recovery sits in the 3.5:1 to 5.5:1 band. Push PA6 or PA66 much beyond about 6:1 and you risk splitting or breakage in the draw zone. The exact drawing medium and temperature should be matched to the grade — this engineering guide to filament stretching covers how hot-water versus hot-air drawing changes the outcome.
For diameter tolerance, high-end brush filament lines use closed-loop laser gauging with dual-axis measurement to hold roughly ±0.002 to ±0.005 mm on precision products. If your target bristle is fine or the brush must trim to a tight specification, closed-loop diameter feedback is not optional — see how to achieve stable monofilament diameter control on a production line to understand why the gauge loop is essential.
Pro Tip: Ask the vendor for the temperature profile and draw-ratio window for each PA grade you plan to run. A line that is only “nylon compatible” in the brochure but lacks a barrier screw or melt pump will fight you on diameter stability from day one.
How Line Design Prevents Specific Nylon Defects
The best way to evaluate a machine is to map each station to the defect it prevents. If a quote skips a station, you inherit the defect on the plant floor.
Defect | Root Cause | Line Design Countermeasure |
|---|---|---|
Bubbles, porosity, die drool | Moisture in hygroscopic resin | Closed-loop desiccant drying to <0.05% at −40°C dew point |
Diameter surging, denier hunting | Screw pulsation, melt pressure drift | Gear melt pump + stable PID zone control |
Ovality, uneven cross-section | Quench temperature drift, turbulence | Tight quench control (±1–2°C), stable bath |
Breakage, necking in draw | Draw ratio too aggressive for melt strength | Multi-stage draw matched to grade, synchronized godets |
Shrinkage, lost curl memory | Residual internal stress | Heat-setting annealing after drawing |
Flattened crimp, poor recovery | Insufficient crimp temperature, no post-cool | Heated gear crimping + immediate cooling |
Nylon-specific depth is worth restating: because the polymer is hygroscopic and thermally sensitive, drying and melt stability carry more weight than they would on a PET or PP line. For a fuller treatment of material selection and crimp control, this nylon brush filament production guide is a useful companion.
Vendor Evaluation: Must-Haves and Red Flags
Once you know your needs, grade, and the line architecture, build an evaluation framework. Separate what is mandatory from what simply sounds good in a brochure.
Must-haves on any nylon brush filament quote:
Single-screw extruder at 30:1 L/D with a barrier screw and wear-resistant (bimetallic) barrel.
Gear melt pump for surge-free, constant metering.
Closed-loop desiccant drying capable of −40°C dew point and <0.05% moisture.
Multi-stage hot drawing with synchronized godet speed control.
Heat-setting annealing oven for dimensional stability.
Closed-loop laser diameter gauging where tolerance matters.
Adequate winder spindle count and winding speed for your output.
Compliant with relevant standards (for industrial equipment, ISO 9001 and CE marking are common expectations).
Red flags / deal-breakers to watch for:
L/D ratio below 30:1 for nylon, or no barrier screw.
No melt pump — expect diameter surging.
A hopper or simple hot-air dryer instead of a closed-loop desiccant system.
No heat-setting or annealing station.
Single-stage drawing only, with no way to adjust draw ratio per grade.
No closed-loop diameter feedback on a fine-filament line.
Questions to Ask Every Vendor
Use these during RFQ and site evaluation. The answers separate an engineered line from a repackaged generic extruder:
What L/D ratio and screw geometry do you supply, and is the barrel bimetallic?
Is a gear melt pump included, and how is melt pressure feedback closed-loop?
What moisture and dew point does your drying system guarantee for PA6, PA66, and PA612?
What temperature profile do you recommend for each PA grade, and is the heating zoned independently?
What total draw ratio does the line support, and can it be tuned per grade without mechanical rework?
How is diameter measured and controlled inline — open loop or closed-loop laser?
Does the line include heat-setting annealing, and at what temperature range?
How many winder spindles, and what maximum line speed does the configuration achieve at my target diameter?
Next Steps
A nylon brush filament extrusion machine is a capital decision, and the difference between a well-configured line and an under-specified one shows up as scrap, downtime, and lost curl memory for years. Start from your needs assessment, verify the grade-specific processing windows against the line’s capability, and hold the vendor to the evaluation framework above.
Changzhou New Liaoyuan Machinery Co., Ltd. (NLY) has engineered monofilament extrusion lines for more than 30 years, with PA6, PA66, and PA612 brush filament configurations built on 30:1 L/D barrier-screw extruders, gear melt pumps, closed-loop desiccant drying, multi-stage hot drawing, and heat-setting annealing. If you are ready to move from specification to a concrete quote, request a line configuration proposal or a technical specification audit, or schedule a Factory Acceptance Test (FAT) sample run on the exact grade and diameter you intend to produce. Comparing a tailored line layout against your requirements list is the fastest way to confirm the investment before you commit.







